
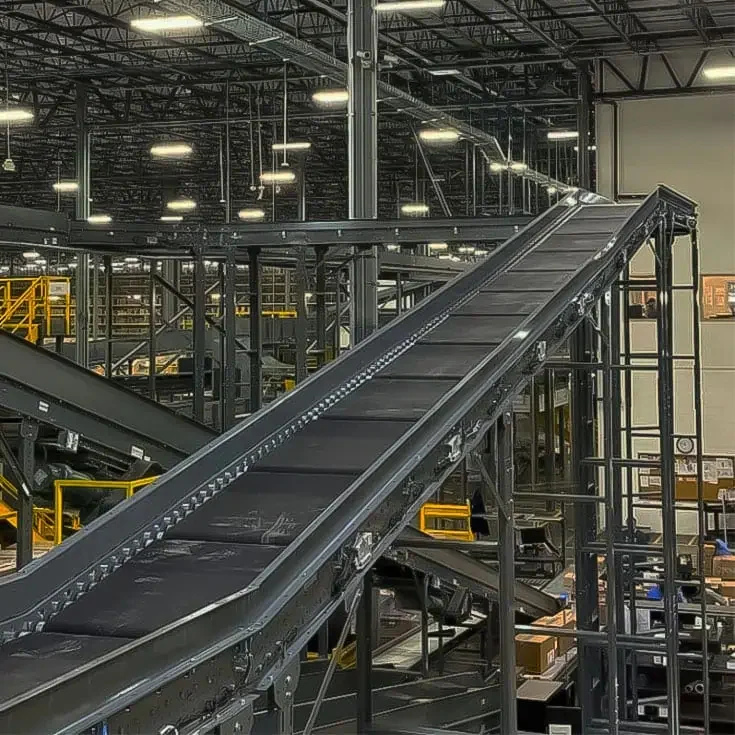
Weekly Highlight: Inclined Conveyor Systems
2-3 Minute Read ⏱ Categories: Conveyor, Material Handling
Can You Take Me Higher?
When working in manufacturing, some of the key qualities you may look for are precision, control, and effectiveness. And for some reason, heights tend to throw a wrench in these well thought out plans.
When having to transport materials throughout a warehouse, the design can often become complex or inefficient. You may have reduced floor space due to heavy machinery transportation, storage systems, or poorly optimized manufacturing equipment. All of this, with the combination of some facilities having elevated stockroom racks, can make the delivery and storage of products difficult. This gap in productivity is where an inclined conveyor system can come into use.
In this blog, we’ll discuss how including an inclined conveyor system can completely change your operation. It not only may change it, but it also reduces the risk of several workplace hazards that may be associated with heights. All these benefits will be mentioned alongside some of the technical aspects that make this unit so useful. Wrapping up, we’ll discuss how we can help your business implement this machinery so you can start achieving more altitude.
What Exactly is Inclined?
Inclined Conveyor Systems are just as simple as they sound; they are units with transportation usually set at 30-35 degrees. They sit around this angle specifically because of how efficient the equipment operates around this rise. They do have the ability to climb higher with cleated designs for different industrial uses.
Other than the height aspect, what other benefit does it offer? Some of the other notable benefits include:
- Adjustable angles
- Customized features
- Meets regulation standards
As seen in this list, what makes this unit great goes just beyond the inclined orientation. But to fully understand its importance, let’s break down these four points even further.
Angles
Not every warehouse needs the same exact equipment in their rotation. Some companies may need higher angles to reach and transport materials. For this reason, we allow the angle of these conveyors to be adjustable to exactly fit your needs. However, this feature does come with its own benefits and drawbacks.
The first thing to mention is the higher your equipment angle, the more powerful motor you’ll need to operate it properly. This may be an extra cost that needs to be considered before purchasing. However, there is an additional benefit that’s included in having this increased height. The bigger the increase comes with more floor space for other warehousing traffic to pass through. This can further increase the benefits of its efficiency and utility.
Custom Features
Along the same line as the adjustable conveyor, there are several different features that you can alter. One of the main ones that is often customized is the size of the equipment. With packages ranging from small boxes to massive pallets, you need a machine that can match your desired attributes.
Regulation Standards
Another great thing about an incline conveyor is that it meets regulation standards for various industries. Industries like food distribution, pharmaceuticals, chemicals, and many others require strict accordance with organizational standards. However, when we design this system, we take into consideration these regulations and craft the safest solution possible.
What Happens When You Buy?
With the benefits we’ve talked about, what exactly does this equate to? Are there any real measurable results from this purchase? While we may not know any issues you face, there is some important data that’s beneficial for everyone to keep track of. With the increase in safety and space this provides, keep track of any differences in reported workplace injuries to see the positive change. It’s also important to note the effectiveness the equipment brings, so keeping tabs on how quickly a product gets transported is helpful as well. Finally, if any safety inspection scores are released, see if any notable changes have occurred.
How Can Russell Conveyor Help?
At Russell Conveyor, we’ve worked with a variety of companies in our 20 plus years of operating. We’re very familiar with the problems that plague modern day manufacturing and aim to help fix them. With our skilled team of engineers and specialists, we strive to bring the correct solution to you. We help you throughout the entire process so you can get exactly what you need. Let today start the pathway to further success and see what we can do for you.
Contact us at (336) 526-3014 or email us at sales@russellconveyor.com to get your free quote now.
Interested in seeing our other selection? Visit our dedicated conveyor systems page.
Want to know more about what makes a good plan turn great? Read our blog on how to make impactful plans.
FAQs about Incline Conveyor Systems
Have any questions about incline conveyors after reading? Here, we’ve answered some of the most common questions we receive.
Most systems operate efficiently up to about 30–35 degrees, though cleated designs can push that higher.
Yes, when built with FDA-approved belt materials and stainless-steel frames, our cleated conveyors meet food-grade standards.
Routine inspections, belt tension adjustments, and lubrication of moving parts are generally all that’s needed. Our designs make upkeep simple and cost-effective.